Purge Oven
Application Note
Removing residual solvents and water quickly is critical in a purge oven. By selecting the right vacuum pump, you can dial in the right combination of temperature and pressure to achieve two critical goals. You will minimize process time by quickly boiling off solvents and water. And you will get the highest product quality by maintaining the integrity of plant oils and terpenes. In addition to finding a pump that gives you the right vacuum level and flow, be sure that you use a pump that is rated for use with the solvents you will be using, and that will hold up over the long term
The Right Vacuum
Chemical compounds such as solvents and water evaporate at specific temperature/pressure points. Water evaporates at 100°C (212°F) at 1 atmosphere, or 1013.25 mbar. Under vacuum (i.e., at lower pressure), any liquid will evaporate at a lower temperature. For example, water evaporates at room temperature if you reduce the pressure to about 23 mbar. Many chemical processes take advantage of this point to evaporate solvents from temperature sensitive materials. Finding the right combination of temperature and pressure allows this drying or evaporation process to move along as fast as possible. If the vacuum is not deep enough, the process will move along slowly. If you use a pump that gives too much vacuum, you can actually boil off your plant oils or your terpenes. This is obviously an expensive mistake. Too much flow can also lead to solvent loss. By fine tuning the vacuum, you will be able to maximize solvent recovery, too. When you choose a pump to run your purge oven, make sure that it provides high flow in the range where butane, ethanol, and water will evaporate. Review published pump curves, or talk with your pump manufacturer to quantify how much flow you’ll be able to rely on.
Find a Reliable Solution
Your vacuum pump will be exposed to all the solvents and water that flow out of the purge oven. So it is critically important that the pump you choose is capable of standing up to long-term exposure to these solvents. Diaphragm pumps can be constructed of chemical-resistant wetted materials to provide outstanding durability. Look for wetted materials to include fluoropolymers like PTFE to maximize the life of the pump. Whatever types of pumps you consider, make sure to ask your pump manufacturer about maintenance requirements, service intervals, and the cost of maintenance. Considering the amount and frequency of preventative maintenance can help you to keep your production up and running and have a significant impact on throughput – and profitability.
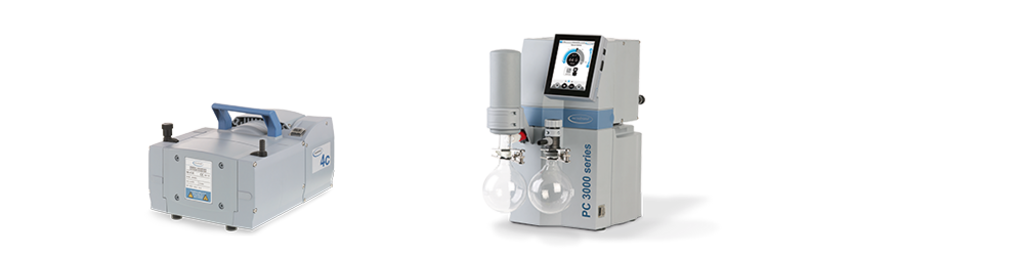
MD 4C NT
1.1 torr ult. vacuum, 63 LPM
• Reliable workhorse pump for ovens and rotavaps
• High flow + Deep vacuum = Fast process
PC 3004 VARIO® select
1.1 torr ult. vacuum, 77 LPM
• Automate drying processes for fastest possible drying time
• VARIO® control holds ultra-precise vacuum, preventing product loss
Purge Oven
Solutions for Purge Ovens
VACUUBRAND® offers many pumps that are well-suited for purge ovens of all sizes. Our chemistry-resistant diaphragm pump technology provides the right level of vacuum in combination with high flow rates that are critical for short process times. Fluoropolymer wetted materials and a durable planar diaphragm design give our pumps industry- leading 15,000-hour typical service intervals, making them the lowest maintenance option on the market. And our intuitive, touch-screen VACUU·SELECT® controller allows you to fine-tune the vacuum level to minimize process time, prevent product loss, and maximize solvent recovery.